30s Guide to Using the Stainless Steel Strap Banding Tool
Author: Site Editor Publish Time: 11-02-2025 Origin: Site
How to Use a Stainless Steel Strap Banding Tool
A manual stainless steel banding tool tensions the band around a pole, bracket, hose, sign, or other assembly, then cuts the tail so the buckle can be locked. Correct installation depends on using a compatible tool, band, and buckle—and on following the finishing method specified for that buckle design.
This guide shows the general sequence for a ratchet-style stainless steel strap banding tool used with uncoated stainless steel band and a matching ear-type stainless steel buckle. Read the instructions for the exact tool and buckle before starting because allowable band width, thickness, tension, and locking method can differ.
■ Before You Start
Stainless steel band edges and freshly cut tails can be sharp. Work on a stable assembly, keep other people clear of the tensioning area, and wear appropriate cut-resistant gloves and eye protection. Inspect the tool, cutter, gripper, band, and buckle before use; replace damaged or mismatched parts rather than forcing them together.
Confirm compatibility: Check the permitted band width and thickness for both the tool and buckle.
Confirm the load: Use the bracket or equipment manufacturer’s band quantity, wrap method, and tension requirements.
Protect the assembly: Make sure the band cannot crush a cable, hose, enclosure, coating, or other sensitive surface.
Check the environment: Select a stainless steel grade and buckle suitable for the corrosion and service conditions.
■ Six Steps for Installing Stainless Steel Banding
1. Measure and cut the band
Wrap a measuring tape around the installation path or calculate the required circumference. Add enough length for the overlap, buckle return, and the tail that the tensioning tool must grip. A tail of approximately 150–200 mm is common for many manual installations, but the exact allowance should follow the bracket, buckle, and tool instructions. Cut the band squarely and control the sharp end.
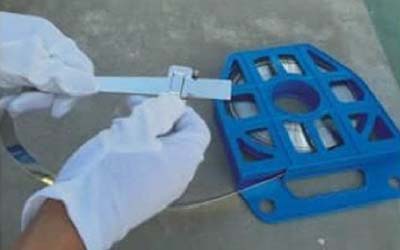
2. Fit the buckle and form the return bend
Slide the buckle onto one end of the band in the orientation shown by the buckle manufacturer. Bend the short end back under the buckle and flatten the return bend so it cannot pull out while tension is applied. Keep the buckle ears accessible for the final locking step.
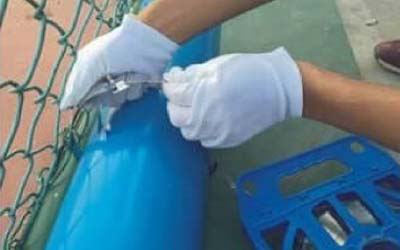
3. Wrap the assembly and thread the free end
Route the band through the bracket or mounting hardware, around the pole or object, and back through the buckle bridge. Keep the band flat and free of twists. If the approved design calls for a double wrap, continue around the object and pass through the buckle again before tensioning. Do not add a second wrap unless the hardware design and installation instructions support it.
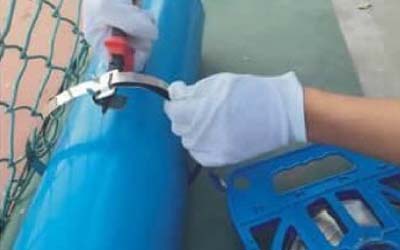
4. Load the tool and tension gradually
Feed the free end into the tool nose and gripper as far as the tool instructions require, positioning the nose close to the buckle without trapping it. Hold the tool square to the band and turn the tension handle with steady, controlled movements. Stop at the specified tension or at the manufacturer’s stated stopping condition. Over-tensioning can deform the mounting hardware, damage the band, or crush the supported component.
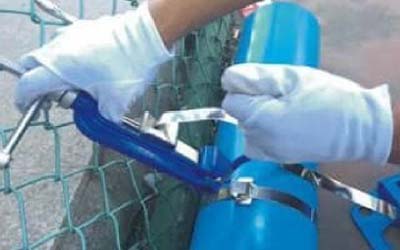
5. Roll over the buckle and cut the tail
For a conventional ear-type buckle system, roll the tool over the buckle while progressively backing off the tension handle. This allows the released band to form the locking bend instead of breaking as the tool pivots. Once the tool is fully rolled over, operate the built-in cutter as directed. Keep hands and nearby cables clear of the cut path and control the offcut.
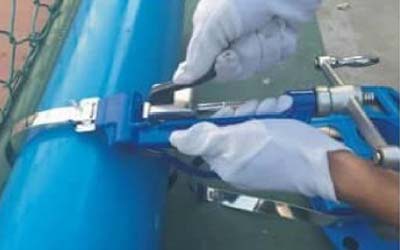
6. Lock the buckle and inspect the finished band
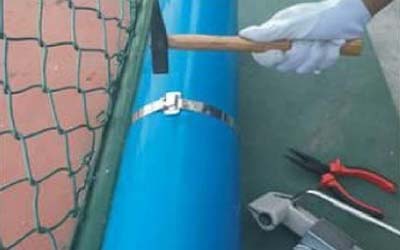
Remove the tool while holding the short band stub in position. For an ear-type buckle that is designed to be hammered closed, press or hammer both ears down evenly over the stub. Other buckle types may use a screw, preformed lock, or a different finishing action, so never substitute the ear-buckle method without checking the buckle instructions.
Inspect the completed band for a flat wrap, fully seated buckle, secure stub, smooth cut end, and correct bracket position. Confirm that the assembly has not shifted and that no cable, hose, coating, or enclosure has been crushed.
■ How Much Tension Should You Apply?
There is no universal “hand-tight” value for every stainless steel banding installation. Required tension depends on band material, width, thickness, buckle type, tool model, bracket design, supported load, pole or object material, and environmental loads such as wind or vibration. Use a calibrated or controlled-tension tool when the project specification requires a defined value.
Do not test the finished band by placing hands beneath a suspended load or by pulling on mounted equipment. Follow the approved inspection method for the installation.
■ Common Installation Mistakes
Using mismatched components: The tool may not grip correctly or the buckle may not lock a band of the wrong width or thickness.
Leaving too little tail: The gripper cannot hold the band securely, making controlled tensioning difficult.
Twisting the band: A twisted band does not seat evenly and can introduce a sharp edge or uneven load.
Failing to back off during roll-over: Keeping full tension while pivoting the tool can break or overstress the band.
Over-tensioning: Excessive force can damage the mounted component, bracket, buckle, or band.
Leaving a hazardous cut end: Finish and position the stub according to the buckle design so it does not create an exposed sharp edge.
■ Tool Inspection and Maintenance
Clean metal particles and dirt from the gripper teeth so the band does not slip. Check the cutter for damage, keep moving parts and the tension screw lubricated as directed by the tool manufacturer, and replace worn grippers, cutters, pins, or handles with the correct parts. Store the tool dry and release tension before storage.
If the tool slips, cuts poorly, binds, or produces inconsistent tension, remove it from service until it has been inspected and repaired. Do not compensate for a worn tool by applying extra force.
■ Frequently Asked Questions
Can one banding tool handle every stainless steel band size?
No. Every tool has a supported band-width and thickness range. The buckle must also match the selected band. Confirm all three components before installation.
Do all buckles need to be hammered closed?
No. Ear-type buckles commonly use ears that are pressed or hammered over the band stub, while screw-lock, center-punch, preformed, and proprietary buckles use different locking methods. Follow the exact buckle instructions.
When is a double wrap needed?
A double wrap may provide greater clamping capability, but it is not an automatic upgrade. Use it only when the bracket, buckle, band, supported load, and installation specification are designed for a double-wrap configuration.
Why does the band slip in the tool?
Common causes include dirty or worn gripper teeth, an incorrectly loaded tail, insufficient engagement in the tool nose, damaged band, or a band thickness outside the tool’s range. Stop and correct the cause instead of applying more force.


 Fiber Optic Tools
Products 6 families
Solutions 6 markets
Resources Tools & docs
Certificate
Certification and compliance references for project review, qualification and purchasing documentation.
 Fiber Optic CableAccess and backbone
 Ethernet CableCat5e to Cat8
 Coaxial CableRF and video signal
 Fire, Security & AlarmSafety systems
 Voice, Audio & VideoSignal cabling
 Power & Control CableEnergy and control
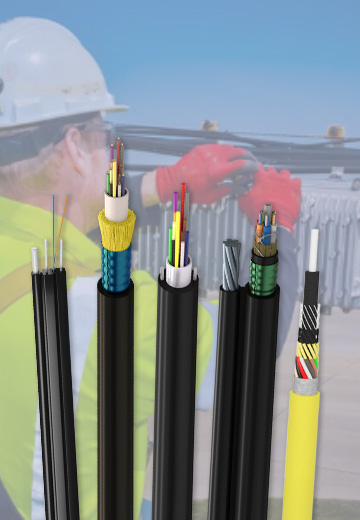
Fiber optic cable systems
Outdoor, indoor, FTTH and distribution cable lines for access networks, backbone routes and campus deployments.
 Telecom & ISP NetworksFTTH, PON, ODN
 Data Center InfrastructureServer room cabling
 Building Low-Voltage SystemsBMS, AV, weak current
 Security & Fire ProtectionAlarm, CCTV, access
 Industrial Automation CablePLC, RS485, fieldbus
 Energy & Power InfrastructureSolar, battery, power
Telecom & ISP Networks
For FTTH / PON access, outdoor fiber deployment, aerial routes, duct routes, direct burial routes, rural broadband and ODN planning.
Tools
Use calculators and planning tools for conduit capacity, PoE voltage drop and fiber optic link loss budget work.